Project stages, LOD and process piping
Ask three piping teams what “LOD 300” means and you may get three slightly different answers. Level of Development (LOD) is a useful shorthand for how complete and reliable a model element is, but it came from the building sector and has been adapted, sometimes loosely, for process plants. This article sets out what the piping model, its deliverables and its checks typically look like at each project stage.
Please read it as a guide, not a standard. Stage names, LOD definitions and the level required at each milestone vary between projects, owners and regions. The project’s BIM execution plan (BEP), model progression specification or contract sets the actual requirement. Where they say something different from this article, they win.
New to the role? Start with Lesson 1: What a Piping Designer Does, which covers the deliverables and project phases this article builds on.
What LOD is really telling you
LOD is less about how detailed an object looks and more about how far others can rely on it. A pipe drawn at the right size in roughly the right place might look finished, but if its route hasn’t been agreed with structural, stress and operations, nobody should be ordering material from it yet. A good way to read an LOD label is: “what decisions can I safely make from this element?”
Stage by stage
The table below is a summary. The sections that follow give more detail.
| Stage | Indicative piping LOD | Typical model content | Typical deliverables | Typical checks |
|---|---|---|---|---|
| Concept / feasibility | LOD 100 | Space reservations, routing envelopes, symbolic main headers | Plot plan options, rough quantities | Fit, safety distances, constructability at a high level |
| BOD / FEED | LOD 200 | Main and critical lines routed at approximate size; racks and corridors fixed; key valves and equipment nozzles placed | Plot plan, equipment layout, rack sections, preliminary MTO, critical-line list | 30%-style layout review, early stress screening, access and escape routes |
| Detailed design, 30% | LOD 200 to 300 | Major lines routed with spec components; equipment and steel firming up | Model review package, updated MTO | Layout and access review, clash trend, spec assignment |
| Detailed design, 60% | LOD 300 | Most lines routed with fittings, valves and inline instruments; primary supports placed; stress-critical lines modelled for analysis | Draft GAs, support list in progress, stress isos | 60% model review, stress results fed back, operability and maintenance review |
| Detailed design, 90% | LOD 350 | All lines complete; supports detailed; interfaces with steel, electrical and instruments coordinated | Near-final GAs, check isos, final MTO | 90% model review, clash resolution to zero, iso checking |
| Issued for construction (IFC) | LOD 350 to 400 | Model frozen for issue; spool breaks, field welds and vendor-confirmed dimensions where required | IFC isos, GAs, support drawings, BOM | Iso release gate, revision control, hold list cleared or recorded |
| Construction | LOD 400 | Changes from site queries and approved deviations | Revised isos, field change records | Change control, re-check of affected lines |
| As-built / handover | LOD 500 (where required) | Model updated to reflect what was actually installed, with agreed attributes | As-built isos and model, data handover to the owner | Field verification, data completeness against the handover requirement |
Concept and feasibility
At this stage the “piping model” may be little more than volumes: a corridor where the main rack will go, a box around a pump group, a line on a plot plan showing that cooling water has to get from A to B. That is a routing envelope, not a route. Its job is to prove the plant fits and to support cost estimates. Nobody should take quantities from it beyond a rough order of magnitude.
Basis of Design (BOD) / FEED
The term Basis of Design is often used for this stage, because its key output is an agreed basis for detailed design. For piping that usually means:
- the plot plan and equipment layout are fixed enough to design against;
- the main racks have levels and widths, often checked with a line-spacing calculation;
- large, expensive or stress-critical lines (hot, high-pressure, large-bore, connected to rotating equipment) are routed early, because they drive the layout;
- a preliminary MTO supports the cost estimate.
Lines here are routed at approximately the right size and position, but fittings may be generic and supports are usually only implied.
Detailed design: 30%, 60% and 90%
This is where the model moves from “routed” to “routed with real components”.
- Fittings and valves are placed from the piping specification, which is loaded as data, so sizes, ratings and end types come from the spec rather than being drawn by hand.
- Instruments move from placeholders to tagged inline items with vendor dimensions where they are known (control valves, flow elements, relief valves).
- Supports go from a few primary supports at 60% to a full, detailed set by 90%.
- Stress-critical lines are modelled early enough for analysis, and the results (loop sizes, support types, nozzle load fixes) come back into the model before 90%.
Each review is a gate. The model is checked against agreed criteria, and comments are tracked to closure, before the work moves on. The Model Review Checklists give a starting list of what to check at 30%, 60% and 90%.
Issued for construction (IFC)
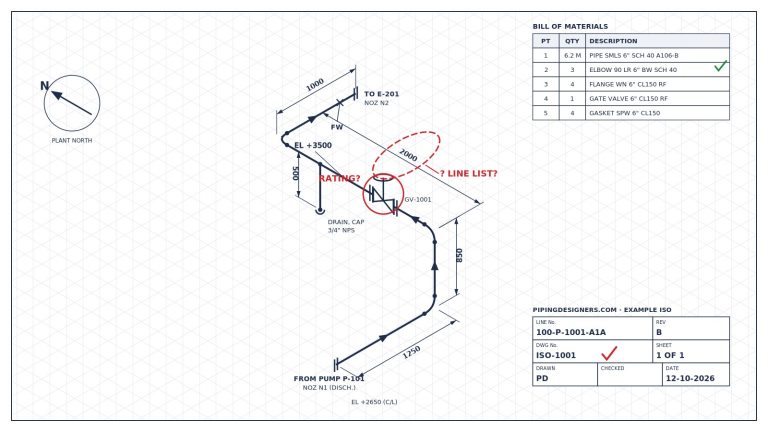
IFC is a formal issue, not just a further percentage. Isos, GAs and the BOM are generated from the model and released through a defined gate. Typical release checks cover spec compliance, dimensions, welds, supports, open holds and revision status. Our Isometric Release Gate Checklist gives one structured way to do this.
Whether the model reaches LOD 400 (fabrication-level) at IFC depends on the contract. On some projects the fabricator adds spool and weld detail in its own system; on others the design model carries it.
Construction
The model doesn’t stop at IFC. Site queries, clashes found in the field and approved deviations all need to go back into the model under change control, or the next revision of the iso will undo the fix.
As-built and handover
LOD 500 is sometimes read as “even more detail”. It is better read as “verified against what was installed”. Owners increasingly want a model and dataset they can run the plant from: tags, line numbers, specs, test records and links to documents. The handover requirement should say exactly which attributes and which accuracy are needed. Laser scanning is often used to verify or capture as-built conditions, especially on brownfield work.
Some typical examples
| Element | Early (LOD 100 to 200) | Mid (LOD 300) | Late (LOD 350 to 500) |
|---|---|---|---|
| Line routing | Envelope or single-line route | Routed at correct size with spec fittings | Final route coordinated, spools defined, as-built verified |
| Valves | Location implied by the P&ID | Spec valves placed with correct face-to-face and handwheel orientation | Vendor-confirmed dimensions, operator access verified |
| Instruments | Placeholder or none | Tagged inline items, approximate dimensions | Vendor data, removal clearances, as-built tags |
| Supports | Implied, or rack beams only | Primary supports and anchors placed | All supports detailed, linked to support standards, loads checked |
| Stress-critical lines | Identified on a critical-line list, early route | Modelled for analysis, results incorporated | Final analysis matches the issued model |
Where the tools help
A few PipingDesigners tools fit naturally at particular stages:
- BOD / FEED: Line Spacing Calculator and Pipe Rack Designer for rack widths and levels; Pipe Loop for early flexibility screening.
- Detailed design: Pipe Span Calculator and Support Details for supports; Line BOM for quantities.
- Reviews and IFC: Piping Design Checklists for model reviews and the Isometric Release Gate Checklist for iso release.
These are screening and checking aids. They don’t replace project calculations or the responsible engineer’s judgement.
A word on automation and AI
Design software already automates a great deal: spec-driven placement, clash detection, iso and BOM generation. AI-assisted tools are starting to help with routing suggestions, model checking and finding gaps between the P&ID, line list and model. That is promising, particularly for catching inconsistencies early. The principle doesn’t change, though: whatever generated the content, a competent person reviews it at each gate and signs it off, and the LOD a model claims should reflect checked work, not just what the software produced.
Summary
- LOD tells you how far you can rely on a model element, not just how detailed it looks.
- Piping typically moves from envelopes (LOD 100) through routed lines (LOD 200) to full spec components and supports (LOD 300 to 350), fabrication detail (LOD 400) and verified as-built (LOD 500).
- Stress-critical and large lines are routed early because they shape everything else.
- The project’s BIM execution plan or contract defines the real requirement. This article is only a typical picture.
Your view? LOD practice varies a lot between companies and regions. How does your project define LOD for piping, and what would you add or change here? Tell us in the comments below.